
Testing & Laboratory
Vibration and Shock
With its subgroups, experiments and associated standards.
Request a QuoteScope
Subgroups within Vibration and Shock
Each group lands in its own section on the same page; The full list of experiments is there.
Vibration and shock testing
 Sine VibrationIEC 60068-2-6
- Random VibrationIEC 60068-2-64
- Random VibrationASTM D4728
 Mechanical ShockUN 38.3
- Mechanical ShockIEC 62133-2
- Mechanical ShockIEC 62619
- Mechanical ShockUL 2580
- Mechanical ShockISO 12405
- Mechanical ShockUNECE R100
- Mechanical ShockMIL-STD-810
 Drop TestASTM D5276
- Drop TestUN 38.3
- Drop TestIEC 62133-2
- Drop TestIEC 62619
- Drop TestUL 2580
- Drop TestISO 12405
- Drop TestUNECE R100
- PyroshockMIL-STD-810
- Gunfire VibrationMIL-STD-810
- Sine-on-Random
- Random-on-Random
 Resonance Search
- Resonance Dwell
- Classical Shock
- Half-Sine Shock
- Sawtooth
- Trapezoidal Shock
 Transportation Vibration
- Bump
Vibration and Shock — What Does This Testing Field Cover?
The section below describes how the field of Vibration and Shock works. The conditions, sample requirements and acceptance criteria of the individual tests in this field are given on the relevant test pages.
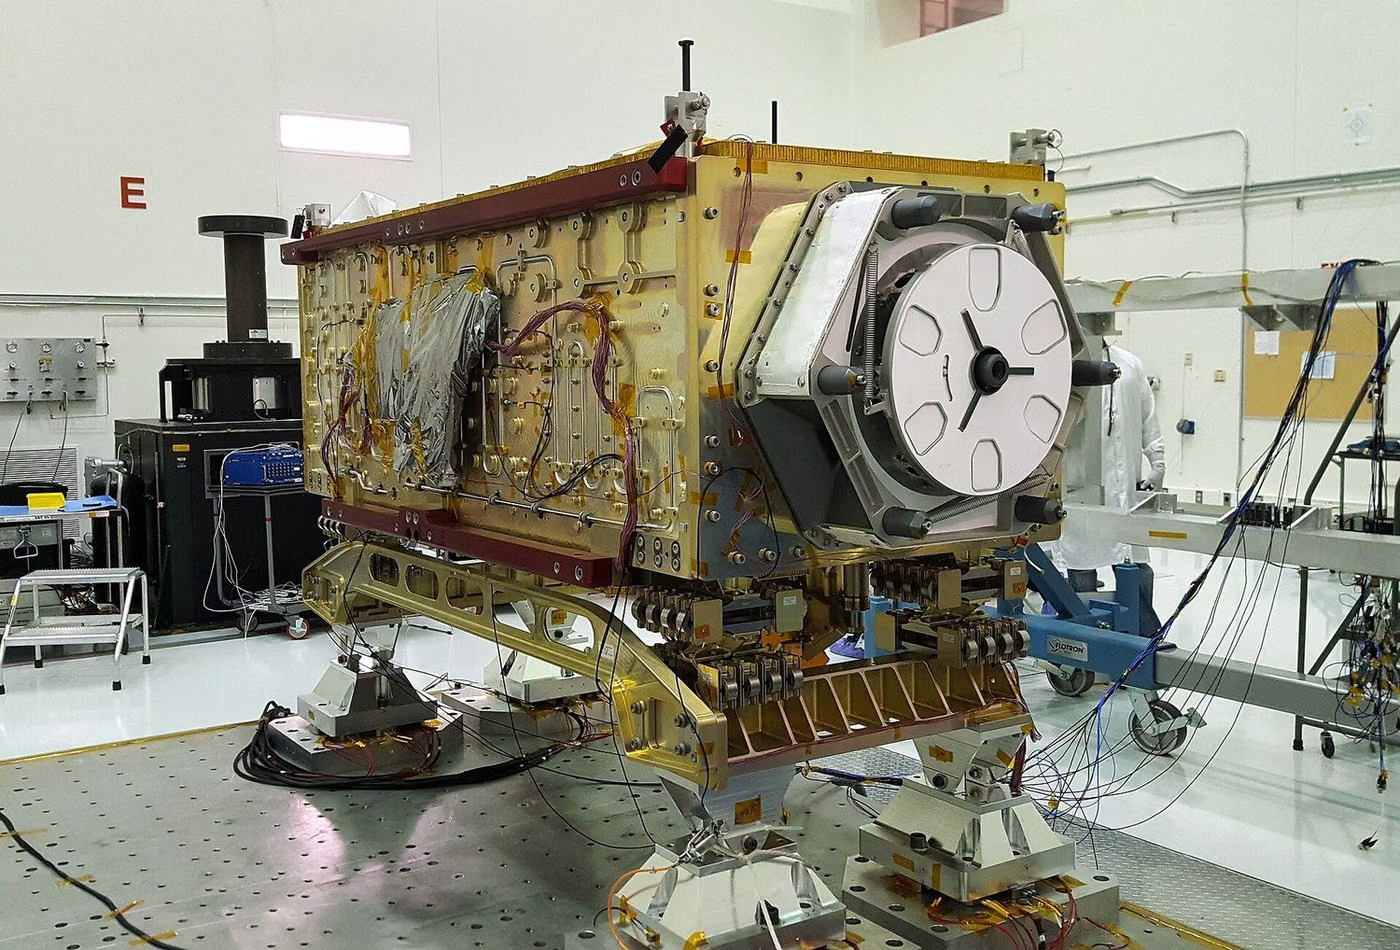
Vibration and shock testing shows whether a product withstands mechanical dynamic loads. The two phenomena are distinct: vibration is a continuous and repeated loading, while shock is a single instantaneous impact at high acceleration. They produce different failure modes and are required separately.
The failure produced by vibration is FATIGUE: a solder joint cracks, a cable sheath abrades, a screw loosens, a connector loses contact. The failure produced by shock is FRACTURE: a brittle component shatters, a bracket breaks, a board comes out of its holder. Testing a product under vibration therefore does not show that it also withstands shock.
Vibration is applied in three forms, each giving different information. Sine vibration sweeps at a single frequency; it is used to find the resonant frequencies of the product and is very valuable at the design stage. Random vibration represents the broadband nature of the real environment and is preferred as evidence of durability. Sine-on-random and random-on-random profiles simulate together the broadband noise superimposed on dominant frequencies from engines and rotors — this is necessary in helicopter and turboprop applications.
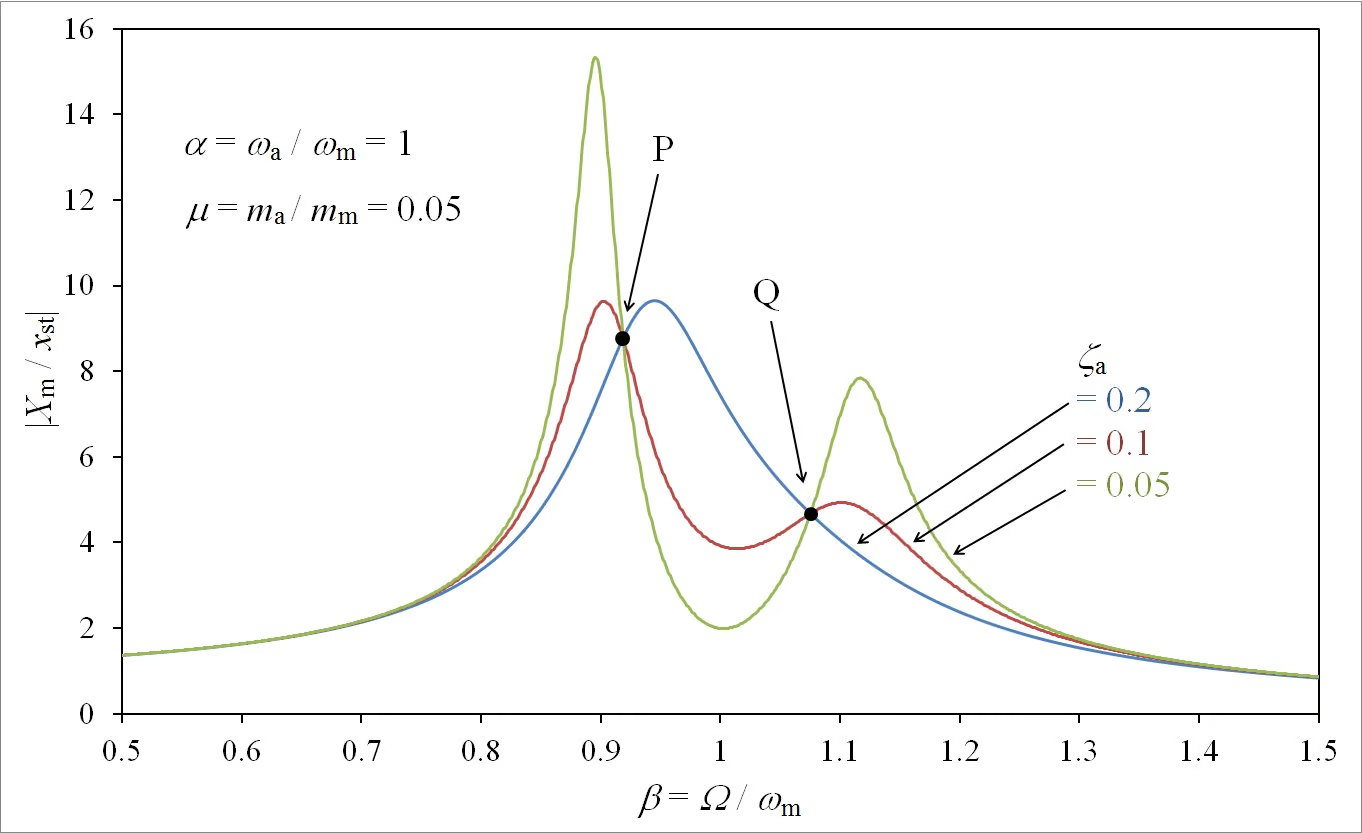
RESONANCE is the concept at the centre of the field. Every structure has its own natural frequencies; as the excitation frequency approaches one of them the amplitude grows and the product is exposed to an acceleration many times the input level. A resonance search is therefore carried out before the test, and a design change often takes the form of shifting the resonance rather than lowering the level.
In this family the FIXTURE is part of the result, and this is the most frequently overlooked point. How the specimen is attached to the shaker directly changes the energy transmitted and the resonance behaviour. A poorly designed fixture brings its own resonances into play and imposes a load the product would not otherwise see, or conversely damps the real load and protects the product. Results obtained with different fixtures cannot be compared.
The choice of measurement point also determines the result. The control accelerometer is placed on the fixture and monitoring accelerometers at critical points of the product; the report must document these positions. Accelerations measured at different points in the same test can differ markedly.
Profiles are divided by application area: transport vibration (packaging and shipping), vehicle vibration (by mounting location), rail (EN 61373 categories), aviation (DO-160 sections), military (MIL-STD-810 methods) and battery transport (UN 38.3 T3). The same product passes through different profiles under different programmes.
Method groups in this field
Sine vibration
Determining resonances by frequency sweep and withstand at defined frequencies; the most informative test at the design stage.
Random vibration
Durability with a broadband power spectral density profile; the approach that best represents the real environment.
Combined profiles
Sine-on-random and random-on-random; for dominant frequencies arising from rotating machinery.
Classical shock
Defined acceleration and duration with half-sine, sawtooth and trapezoidal pulse shapes.
Free fall and toppling
Realistic drop scenarios arising from handling; decisive for portable products.
Resonance search and monitoring
Detection of structural change (cracking, loosening) by sweeps before and after the test.
Commonly confused in this field
- Shock and vibration are not the same test; one produces fracture and the other fatigue, and they are required separately.
- A report that does not document the fixture cannot be compared; a fixture can bring its own resonance into play.
- Levels come from the product standard or the programme specification; the standard does not define a single universal level.
- Without a resonance sweep before and after the test, structural damage can go unnoticed; the product may appear to work while being cracked internally.
- The position of the measurement point must be reported; accelerations measured at different points in the same test differ markedly.
- If the product is not operated during the test, intermittent loss of contact remains invisible.
Which decisions these results support
- Verification of transport and in-use durability
- Transport and vehicle vibration conformity for batteries
- Rail, aviation and defence qualification files
- Root cause analysis of solder, connector and joint failures
- The decision to shift a resonance through a design change
Related standards
Sectors
In which sectors is Vibration and Shock used?
Automotive
Automotive Testing · EMC / EMI Testing · Vibration and Shock
Explore
Aerospace
Aerospace Testing · Environmental and Climatic Testing · Vibration and Shock
Explore
Defence
Defence Testing · Environmental and Climatic Testing · Vibration and Shock
Explore
Railway
Railway Testing · Fire Testing · EMC / EMI Testing
Explore
Logistics
Packaging Testing · Food Testing · Environmental and Climatic Testing
Explore
Vibration and Shock quote
Tell us your product and the applicable standard; we'll share the timeline and sample requirements in writing.