
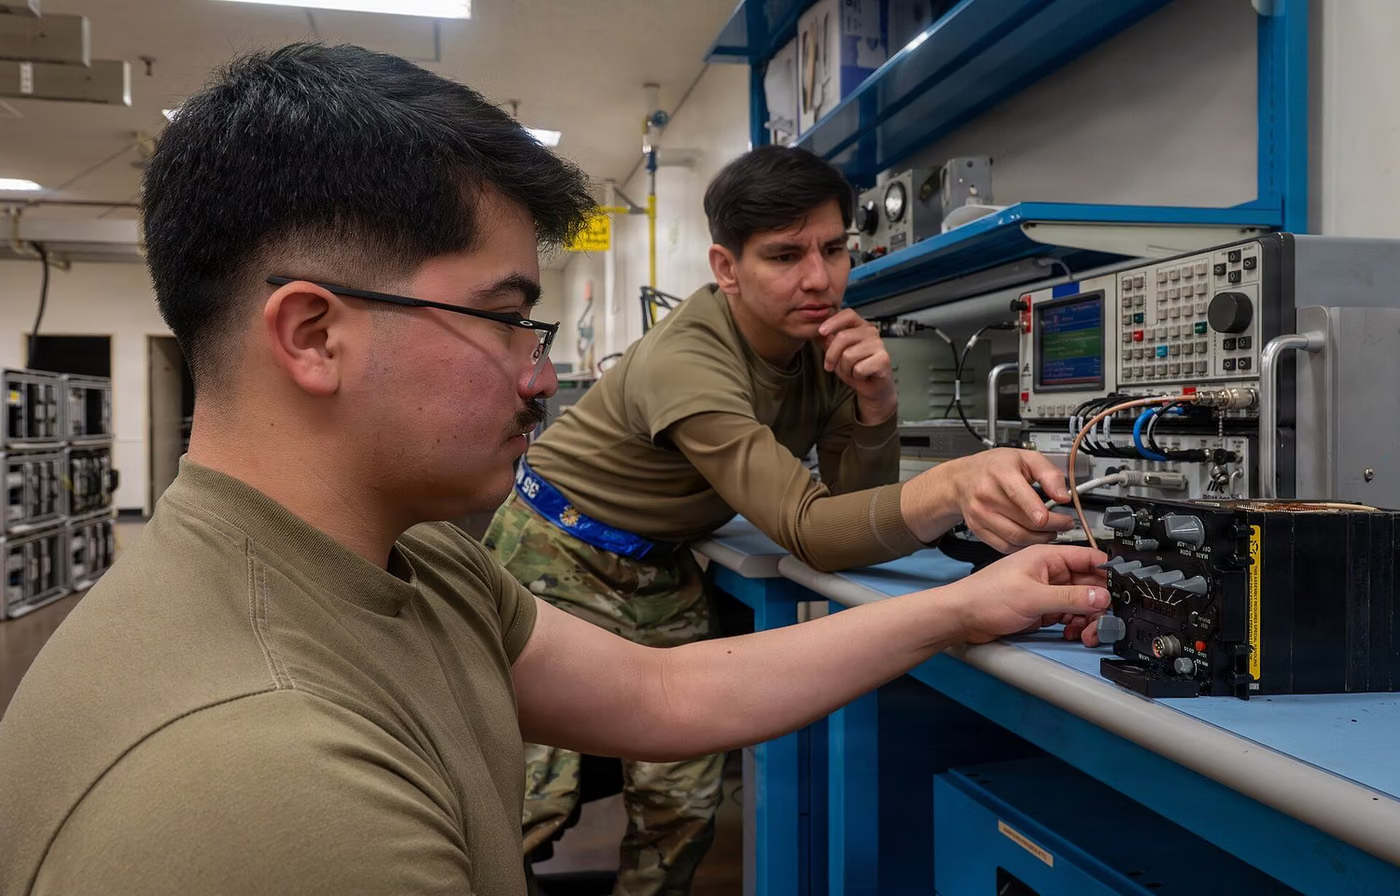
What Is Induced Signal?
This test is carried out within the scope of Chapter 19 (“Induced Signal Susceptibility”) of the RTCA DO-160 “Environmental Conditions and Test Procedures for Airborne Equipment” standard to evaluate the immunity of the equipment to magnetic and electric field-induced signals induced in the cable bundles. DO-160 is the exact same text as EUROCAE ED-14 and is recognized by ISO as ISO 7137.
Purpose of Induced Signal
The aim is to certify that aviation equipment meets the requirements regarding the evaluation of immunity to magnetic and electric field-induced signals induced in the equipment's wiring harnesses in flight and ground conditions and to complete the equipment qualification.
Which Products Is Induced Signal Applied To?
- Avionics units and displays
- In-flight electronic equipment
- Communication and navigation devices
- Cabin and cargo compartment equipment
- Sensors and actuators
In Which Sectors Is Induced Signal Used?
Standards Related to Induced Signal
- RTCA DO-160Environmental conditions and test methods in aviation equipment test
- EUROCAE ED-14
- ISO 7137
Induced Signal Conditions
- Kategoriler
- Z, A, B... depending on aircraft type
- Kaynaklar
- Magnetic field, electric field and cable-induced induction
- Frequency
- Grid frequency and harmonics
- Application
- With coil or parallel cable close to the wiring harness
Equipment for Induced Signal
- Induction coil and cable layout
- Signal generator and amplifier
- Function monitoring
Sample Requirements for Induced Signal
- Cable bundles must be identified
- Category must be defined
- Function monitoring must be set up
Duration of Induced Signal
It depends on the number of cables; typically half to one business day.
Induced Signal Procedure
- 1Categories and levels are determined.
- 2Induction scheme is applied to the wiring harness.
- 3Frequencies are scanned.
- 4Repeated for each cable.
- 5The function is monitored.
Induced Signal Acceptance Criteria
The acceptance criterion is that no functional impairment occurs.
Evaluation of Results
Shielding and cable separation directly affect the outcome of this experiment.
Induced Signal Report
- Applicable standard, revision and Part 19
- Selected equipment category and justification
- Applied conditions and measurement results
- Function monitoring method and observations
- Environmental Qualification Form (DO-160 Environmental Qualification Form) entry
Accreditation
EUROLAB holds internationally recognised accreditation obtained from accreditation bodies party to the IAF and ILAC multilateral recognition arrangements, under ISO/IEC 17025 for laboratory testing, ISO/IEC 17020 for inspection and surveillance, and ISO/IEC 17021-1 and ISO/IEC 17065 for system and product certification. This chain ensures the reports and certificates issued are accepted worldwide.
Whether this test can be offered within accredited scope depends on your product and the standard applied; since accreditation is method-based, the scope is confirmed in writing at the quotation stage.
Scope and authorisationsRelated Regulations
- Aviation equipment qualification requirements
- EASA/FAA certification principles
Aerospace Testing — What Does This Testing Field Cover?
The section below describes the field that the Induced Signal test belongs to; the conditions and acceptance criteria of this particular test are given in the sections above. The scope specific to your product is confirmed in writing at the quotation stage.
Aerospace testing shows that equipment keeps working in the flight environment and provides evidence for the airworthiness file. In this family the acceptable probability of failure is several orders of magnitude lower than in other sectors; this directly determines the scope of testing and the certification burden.
The most distinctive feature of the field is TRACEABILITY. Which melt an aircraft part came from, in which heat treatment furnace and with which cycle it was processed, which operator made the weld and which inspector approved it are all recorded. The test report is one link in this chain; if the chain is broken, the report carries no value on its own.
Environmental qualification runs through RTCA DO-160, with categories selected according to the equipment's MOUNTING LOCATION in the aircraft. A device mounted on the cockpit panel and one mounted inside the wing pass the same section under different categories. When reading a DO-160 report it is therefore essential to know which sections were applied at which categories.
On the software and complex hardware side the approach changes entirely: the evidence is not testing but PROCESS ASSURANCE. DO-178C for software and DO-254 for complex electronic hardware define how the development process is to be run and which evidence is to be produced. Every step, from requirement to code, from testing of the code to coverage analysis, must be traceable. Testing software does not make it certifiable; the process record does.
A separate body of work applies on the material and special process side. AWS D17.1 is used for welding, SAE AMS 2750 for pyrometry in heat treatment and NAS 410 for non-destructive testing personnel. For special processes (heat treatment, coating, welding, NDT, bonding) NADCAP accreditation is effectively mandatory in the supply chain; without NADCAP it is not possible to sell parts to many OEMs.
On the quality system side the AS/EN 9100 series is used: 9100 for manufacturers, 9110 for maintenance organisations and 9120 for distributors. Without these certificates it is practically impossible to enter the aerospace supply chain, and audits are markedly more detailed than in other sectors.
Counterfeit part risk is a subject peculiar to the field. Separate standards and verification methods (visual inspection, X-ray, decapsulation and internal structure examination, XRF) are used to detect counterfeit or reworked parts in the electronic component supply chain.
Space applications add further layers: outgassing in vacuum, radiation tolerance, long-duration thermal vacuum cycling and assessment of single event effects.
Method groups in this field
Environmental qualification
RTCA DO-160 sections: temperature and altitude, vibration, shock, humidity, sand and dust, fungus, salt fog, fluid susceptibility, icing, lightning.
Electromagnetic
The EMC sections of DO-160; MIL-STD-461 and MIL-STD-704 power characteristics on military platforms.
Software and hardware assurance
DO-178C software life cycle and DO-254 hardware design assurance evidence; requirement traceability and coverage analysis.
Materials and welding
Welding qualification under AWS D17.1, mechanical testing of materials, metallography and non-destructive examination.
Special process control
SAE AMS 2750 pyrometry, coating and heat treatment process verification, preparation for NADCAP audits.
Space environment
Thermal vacuum cycling, outgassing, radiation tolerance and acoustic/vibration qualification.
Commonly confused in this field
- There is no such document as a "DO-160 certificate"; DO-160 is a test specification and its output is a qualification report.
- The selection of sections and categories comes from the customer's equipment specification; the laboratory cannot make that selection on its own.
- DO-178C and DO-254 cannot be satisfied by testing; the evidence is the traceability of the development process.
- An AS9100 certificate is not a product approval; it is a quality system certificate and part approval runs separately.
- For special processes, work carried out without NADCAP is not accepted in the supply chain even when it is technically correct.
- MIL-STD-810 and DO-160 are often confused: one is a military and the other a civil aviation specification, and their profiles differ.
Which decisions these results support
- Airworthiness and TSO/ETSO files
- Entry into the aerospace supply chain and supplier approval
- Special process approval and NADCAP preparation
- Determining the impact of a design change on qualification
- Managing counterfeit part risk and component verification
Related Tests
Frequently Asked Questions About Induced Signal
How is the equipment category determined?
The category is selected based on the equipment's mounting location on the aircraft (pressurized/non-pressurized, heated/unheated area) and aircraft type. Category selection directly determines the test conditions and is declared in the qualification form.
Is there any difference between DO-160 and ED-14?
No. RTCA DO-160 and EUROCAE ED-14 are exactly the same text; the two are considered equivalent.