
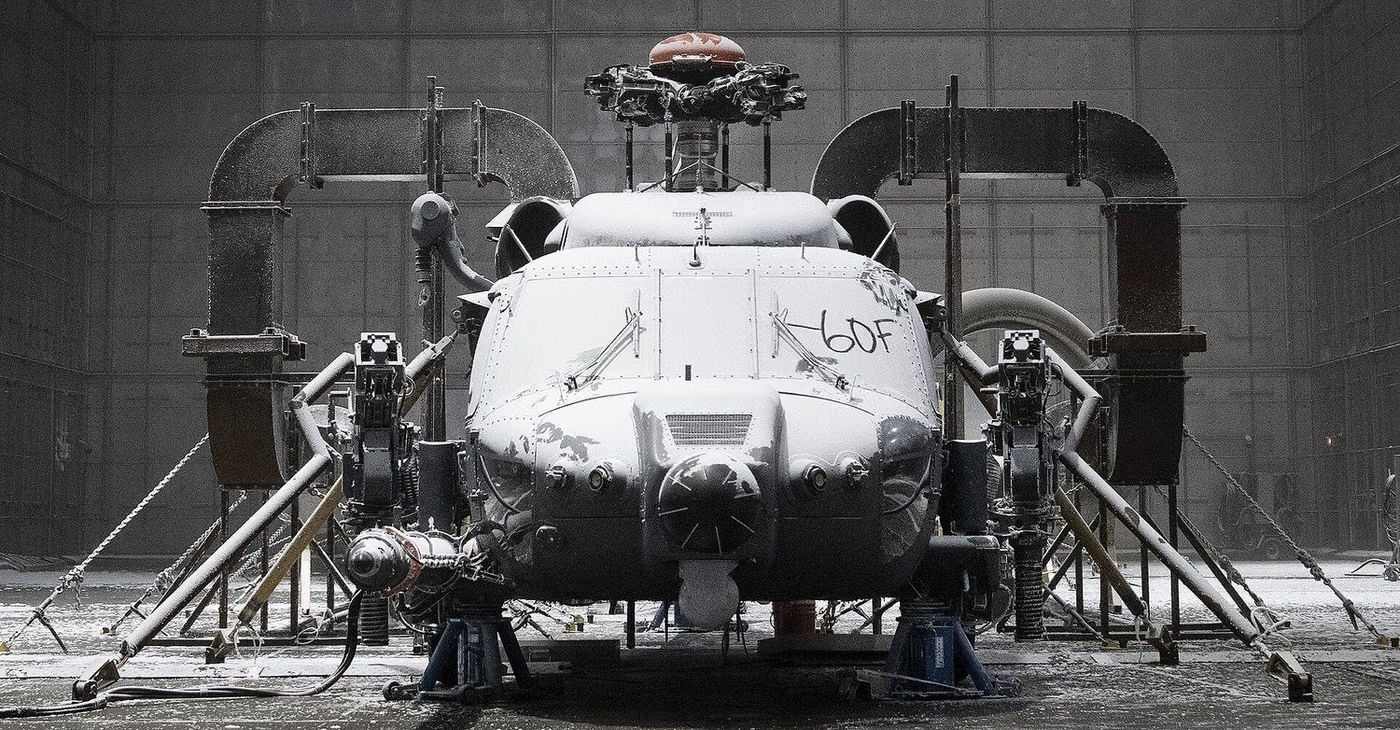
What Is Low Temperature — IEC 60068-2-1?
The low temperature test is an environmental test in which the sample is held at a defined low temperature for a specific duration to assess function and material behaviour. It is defined as the cold test in IEC 60068-2-1.
Purpose of Low Temperature — IEC 60068-2-1
The purpose is to verify that the product operates in cold-climate conditions, materials do not become brittle, and sealing elements retain their function.
Which Products Is Low Temperature — IEC 60068-2-1 Applied To?
- Automotive and rail electronics
- Battery systems
- Outdoor equipment
- Cable and gasket elements
- Aerospace avionics
In Which Sectors Is Low Temperature — IEC 60068-2-1 Used?
Standards Related to Low Temperature — IEC 60068-2-1
- IEC 60068-2-1low temperature (cold) test test
Low Temperature — IEC 60068-2-1 Conditions
- Temperature
- Defined in the product standard; typical ranges −20, −40, −55 °C
- Time
- Defined in the specification; typically 16, 72 or 96 hours
- Operating condition
- Identified separately as operating or off
- humidity control
- Cabin humidity is kept low to prevent icing
Equipment for Low Temperature — IEC 60068-2-1
- Programmable refrigerated temperature chamber
- Multi-channel temperature recording
- Function-monitoring rig
- Dry air supply
Sample Requirements for Low Temperature — IEC 60068-2-1
- The sample must be installed in its typical mounting configuration
- Function must be checked before the test
- Condensation precautions must be taken
- A cold-start scenario must be defined
Duration of Low Temperature — IEC 60068-2-1
Depends on the dwell time defined in the specification; typically one to four days.
Low Temperature — IEC 60068-2-1 Procedure
- 1The sample is placed in the chamber and thermocouples are connected.
- 2An initial function check is performed.
- 3Temperature is lowered to the target value at the defined rate.
- 4It is held for the defined duration; a cold start is attempted if required.
- 5A controlled return to ambient temperature is made and condensation is expected.
- 6A final function check and visual inspection are carried out.
Low Temperature — IEC 60068-2-1 Acceptance Criteria
The acceptance criterion is defined in the product standard: continuity of function or a successful cold start, with no cracking or leakage.
Evaluation of Results
Embrittlement of elastomer and plastic parts, and the drop in display and battery performance, are assessed separately.
Low Temperature — IEC 60068-2-1 Report
- Standard applied
- Temperature, duration and operating condition
- Cold-start result
- Function status and visual inspection
Accreditation
EUROLAB holds internationally recognised accreditation obtained from accreditation bodies party to the IAF and ILAC multilateral recognition arrangements, under ISO/IEC 17025 for laboratory testing, ISO/IEC 17020 for inspection and surveillance, and ISO/IEC 17021-1 and ISO/IEC 17065 for system and product certification. This chain ensures the reports and certificates issued are accepted worldwide.
Whether this test can be offered within accredited scope depends on your product and the standard applied; since accreditation is method-based, the scope is confirmed in writing at the quotation stage.
Scope and authorisationsRelated Regulations
- Automotive and rail equipment specifications
- Aerospace equipment requirements
Environmental and Climatic Testing — What Does This Testing Field Cover?
The section below describes the field that the Low Temperature test belongs to; the conditions and acceptance criteria of this particular test are given in the sections above. The scope specific to your product is confirmed in writing at the quotation stage.
Environmental testing shows whether a product withstands ambient factors such as temperature, humidity, pressure, solar radiation, dust, water and corrosive atmospheres. The aim is not to break the product but to bring forward, in ACCELERATED form, the conditions it will meet over its life.
Test profiles are derived from the product's real exposure, and that derivation is the actual engineering work of the field. A device operating in an enclosed office and one mounted on a pole are not tested with the same profile. The IEC 60068 series defines general methods, MIL-STD-810 military profiles, RTCA DO-160 aviation profiles and the ISO 16750 series location-based automotive profiles. A test applied without a profile selection produces both unnecessary cost and false confidence.
Temperature tests simulate three separate phenomena and all three produce different failure modes. Steady high/low temperature tests whether the material can operate at that temperature. Temperature CYCLING creates fatigue at joints between materials with different expansion coefficients — solder cracks appear here. Thermal SHOCK intensifies this effect through an abrupt transition.
There is a distinction in humidity testing too. Steady damp heat shows the diffusion of moisture into the material and its effect on insulation properties. Cyclic damp heat creates condensation: water droplets form on the cooling surface, and this is far more aggressive than dry humidity. Water ingress into enclosures, increased leakage current and corrosion usually appear in the cyclic test.
Dust and water protection is a separate body of work and is expressed by the IP code. The point to note here is that an IP test is not a DURABILITY test: it shows that protection is provided under defined and short-duration conditions, not resistance to long-term immersion or pressure washing.
The most common mistake in this family is translating a test result directly into a LIFE PREDICTION. Accelerated tests are designed for comparison and design verification; a reliable conversion between hours in a chamber and years in the field can only be established with a material-specific acceleration model calibrated against field data.
Functional monitoring determines the value of the test. Keeping a product in a temperature chamber and then switching it on does not show what happened DURING the test. In critical applications the product is operated throughout the test and its parameters are monitored; intermittent faults that appear and disappear can only be caught this way.
Method groups in this field
Temperature
Dry heat, cold, change of temperature and thermal shock; steady and cyclic profiles.
Humidity
Steady damp heat and cyclic damp heat; cycles with condensation are more aggressive.
Water and dust
IP protection tests: dripping, spraying, jets, immersion and dust tightness.
Radiation and ageing
Accelerated ageing by xenon arc and fluorescent UV, solar radiation simulation.
Pressure and altitude
Low pressure (altitude) and rapid pressure change tests.
Corrosive atmosphere
Salt spray, mixed flowing gas corrosion (simulating industrial atmospheres), mould and fungus tests.
Commonly confused in this field
- Test duration cannot be converted into field life; a conversion made without an acceleration model is misleading.
- Temperature cycling and steady temperature produce different failure modes; neither replaces the other.
- If the product is not operated during the test, intermittent faults remain invisible; functional monitoring determines the value of the test.
- IP protection is not evidence of durability; it shows protection under defined and short-duration conditions.
- A test applied without profile selection both increases cost and gives false confidence.
- The mounting and orientation arrangement affects the result; the report must document it.
Which decisions these results support
- Design verification and qualification
- Declaration of the protection class and operating temperature range
- Reproducing field failures in the laboratory and root cause analysis
- Supplier component approval
- Decisions on warranty period and storage conditions
Related Tests
Frequently Asked Questions About Low Temperature — IEC 60068-2-1
According to which standard is Low Temperature made?
Low Temperature is executed in scope IEC 60068-2-1, ISO 16750-4, MIL-STD-810 Method 502 and RTCA DO-160 Section 4. The limit values and acceptance criteria to be applied are defined in the product standard; The version valid for your product is confirmed in writing at the offer stage.
Which products does Low Temperature apply to?
Mainly applied to Automotive and rail electronics, Battery systems, Outdoor equipment, Cable and gasket elements and Aerospace avionics. Whether your product is included in the scope is determined by examining its technical specifications and intended use.
Under what conditions is Low Temperature done?
The determining parameters are: Temperature — Defined in the product standard; typical ranges −20, −40, −55 °C, Time — Defined in the specification; typically 16, 72 or 96 hours and Operating condition — Identified separately as operating or off. The full terms are in the "Test Conditions" section on the page and vary depending on the product standard.
What kind of sample is needed for Low Temperature?
The sample must be installed in its typical mounting configuration, Function must be checked before the test and Condensation precautions must be taken. The number of samples is determined according to the product standard and the scope to be reported.
How long does Low Temperature take?
Depends on the dwell time defined in the specification; typically one to four days. This duration belongs to the experiment itself; sample preparation, queuing and reporting are also evaluated. A realistic schedule for your product is given in the offer.
What is the Low Temperature result called "appropriate"?
The acceptance criterion is defined in the product standard: continuity of function or a successful cold start, with no cracking or leakage.